


- By h3si5
- August 22, 2026
- 0 Comment
Unlock Massive Growth with These 5 Essential Mineral water plant machinery Upgrades
Mineral water plant machinery is the very backbone of any profitable, high volume packaged drinking water business. In a fast-growing, competitive beverage market, the choice of the right industrial equipment is the difference between a smoothly running and efficient production line and one plagued by constant bottlenecks and high operating costs.
The Evolution of the Packaged Drinking Water Industry
To enter or grow in the commercial machinery mineral water segment, you need precision, strict regulatory compliance and heavy duty reliability. Today consumers expect crystal clear and safe hydration in perfectly bottled form, and local and international food safety authorities enforce strict quality control standards. Faced with these two pressures, business owners cannot afford to be using outdated setups or sub-standard equipment. Jai Sat Packaging Provides Essential Mineral Water Plant Machinery Upgrade For Massive Growth. Increase production efficiency, ensure pure water quality and maximize your profits. Equipment is used to convert raw groundwater or city water into clean drinking water that can be packaged in bulk and sold to the general public.
At Jai Sat Packaging, we have invested in a modern, fully integrated processing plant, where every stage of filtration and deep purification to the final automated capping is performed with the highest precision. But technology moves quickly, and an old, unchanged production line can greatly reduce your market share. To stay competitive, plant owners need to constantly re-assess their setup and make targeted equipment upgrades with industry leaders like Jai Sat Packaging.
Upgrade 1: Advanced Multi-Stage Pre-Treatment and Filtration Systems
Switch to Automated Backwash Filters New age Multi-Grade Sand Filters (MGF) and Activated Carbon Filters (ACF) with automatic pneumatic or motorized multiport valves ensure consistent cleaning of the media without heavy manual labor.
Precision Micron Bag Filtration Upgrading to multi-stage bag or cartridge filter housings ensures that suspended solids, silt, and fine rust particles are trapped effectively before reaching high-pressure pumps, protecting your core investment.
Upgrade 2: High-Efficiency Reverse Osmosis (RO) and Energy Recovery
The purification core is the heart of any water treatment plant. Traditional RO systems use a lot of electricity and produce a lot of waste water. Both impact your bottom line directly.
- High-Rejection Composite Membranes High performance membrane elements allow for better reduction of total dissolved solids (TDS) at lower pressure settings.
- High-pressure pumps with variable frequency drives (VFDs) – we install VFDs to vary the speed of the pump to match the actual demand for water, dramatically reducing energy use and mechanical strain on your main motors.
Upgrade 3: Next-Generation Disinfection with Ozone and UV Sterilization
Microbiological safety must be guaranteed, no compromises. A small amount of contamination can lead to massive product recalls, heavy fines and permanent damage to a brand.
High Output Ozone Generators: When you upgrade your ozonation system, the dissolved ozone is of a high concentration and this not only sterilizes the water but also sanitizes the inner walls of storage tanks and bottles right before they are sealed.
Advanced UV Sterilizers: Integrated high-intensity ultraviolet chambers instantly disrupt the DNA of microbes, creating a chemical-free secondary barrier against bacteria and viruses.
Upgrade 4: High-Speed Automated Rinsing, Filling, and Capping Lines
When the water is purified it must be packed quickly and hygienically. Manual or semi-automated filling lines introduce human error, inconsistent liquid levels and high rates of product spillage.
The Mineral water plant machinery Rotary monoblock systems. The move to integrated rotary rinsing, filling and capping monoblocks is a boon to the workflow for small polyethylene terephthalate (PET) bottles (500ml to 2 liters).
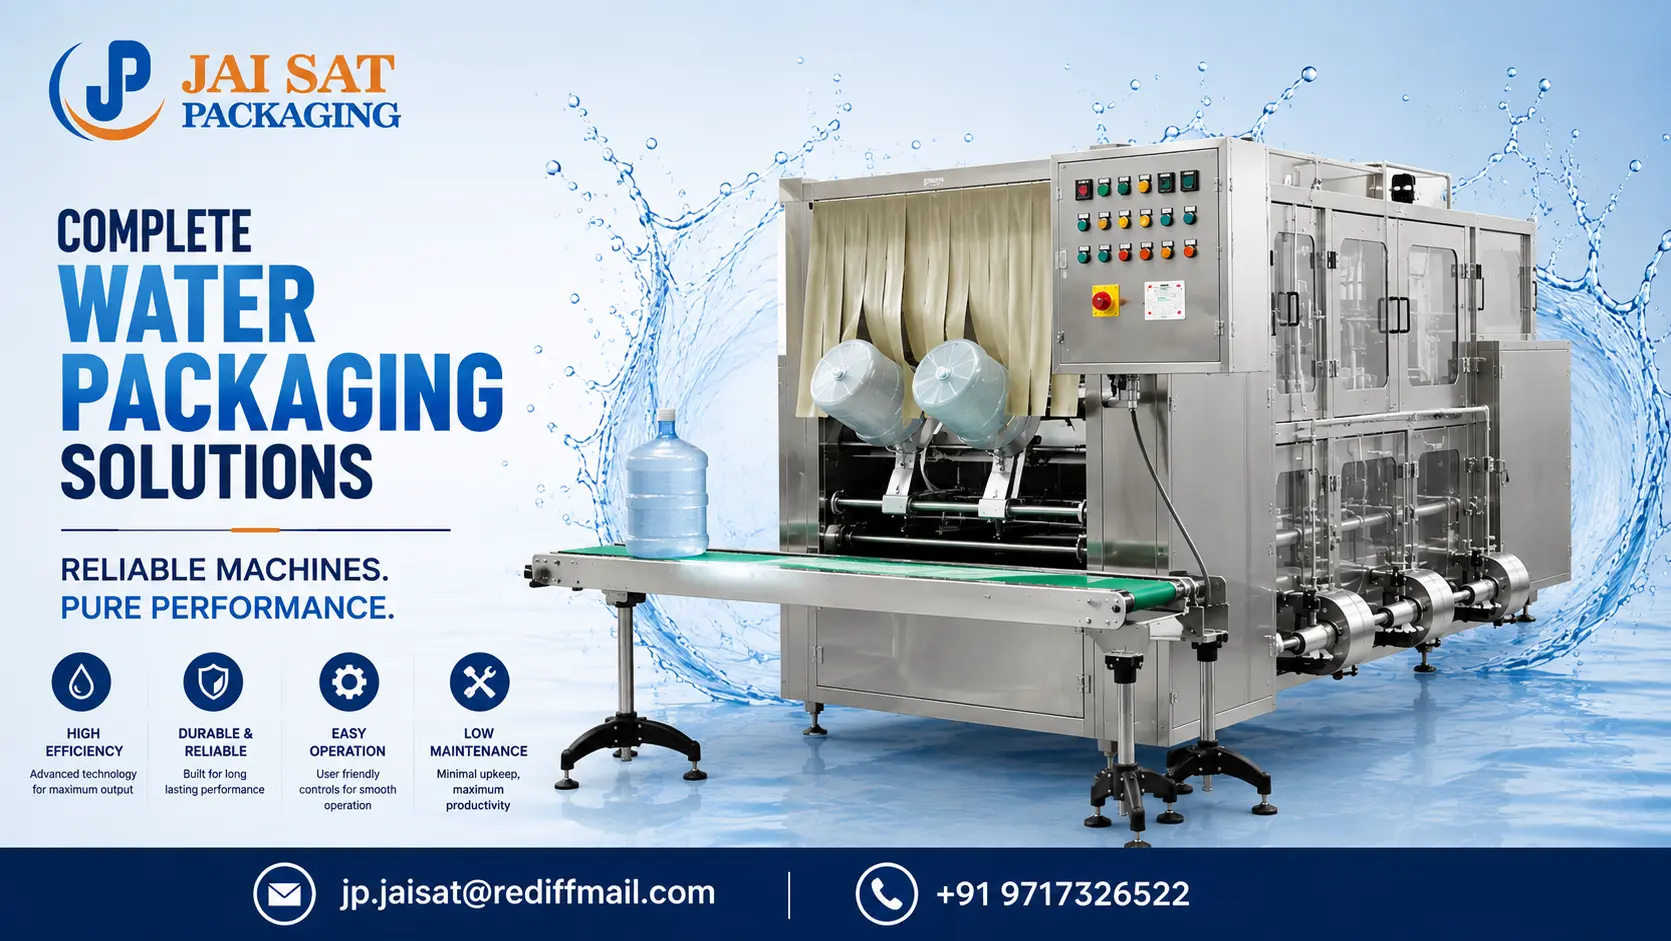
Commercial water delivery operations can eliminate production bottlenecks by investing in stainless steel automatic 20L jar washing, rinsing and filling machines capable of outputting up to 1200 jars per hour (JPH). Heavy-Duty 20-Liter Jar Processing Lines
Upgrade 5: Intelligent PLC Automation and Touchscreen Interfaces
The final piece of the puzzle is facility-wide visibility and control. Modern industrial plants rely heavily on smart automation to measure performance, fluid levels and to prevent catastrophic equipment failures.
Centralized Control Panels Replacing legacy systems with Programmable Logic Controller (PLC) systems with user-friendly touchscreen interfaces allow operators to monitor flow rates, tank levels and filling accuracies in real time.
Error Detection and Automated Shutoffs Automation has decreased the number of manual touch points for operators, providing accurate control of the volume of liquid, while still providing ±1% filling accuracy and reducing the cost of product wastage.
Best Practices for Plant Maintenance and Upgrading
To execute these upgrades effectively, you need to plan and organize your facility management strategically: Complete Water Quality Audit – Before buying new equipment parts, make sure the specs of the Unlock massive growth with essential Unlock massive growth with essential mineral water plant machinery upgrades. Boost production efficiency, ensure pure water quality, and maximize profits. upgrades. The Mineral water plant machinery Boost production efficiency, ensure pure water quality, and maximize profits.correspond to your exact chemical and physical profile by testing your source of raw water in detail.
Phased Implementation : Replace equipment and change pipes during scheduled maintenance outages or during off peak hours, so that commercial operations are not totally shut down.
Operator Training Programs: Provide your technical staff with professional training to work with new PLC software, manage automated clean-in-place (CIP) cycles and perform routine preventive maintenance
Conclusion
Scaling a beverage business means looking forward to infrastructure and capital expenditure. Implementing these five key improvements into your operations will lead to long-term equipment reliability, reduced energy consumption and pure product quality. With Jai Sat Packaging, upgrade your facility and your brand will be able to meet the rising demand in the market and maintain the profitability of Mineral Water Plant Machinery in the Packaged Drinking Water Industry.
